Research / Sector playbook
AI Readiness for a Regional Manufacturer: Follow the Production Order
Assess manufacturing AI readiness by tracing a production order through scheduling, quality, maintenance, and ERP records before choosing a model or vendor.
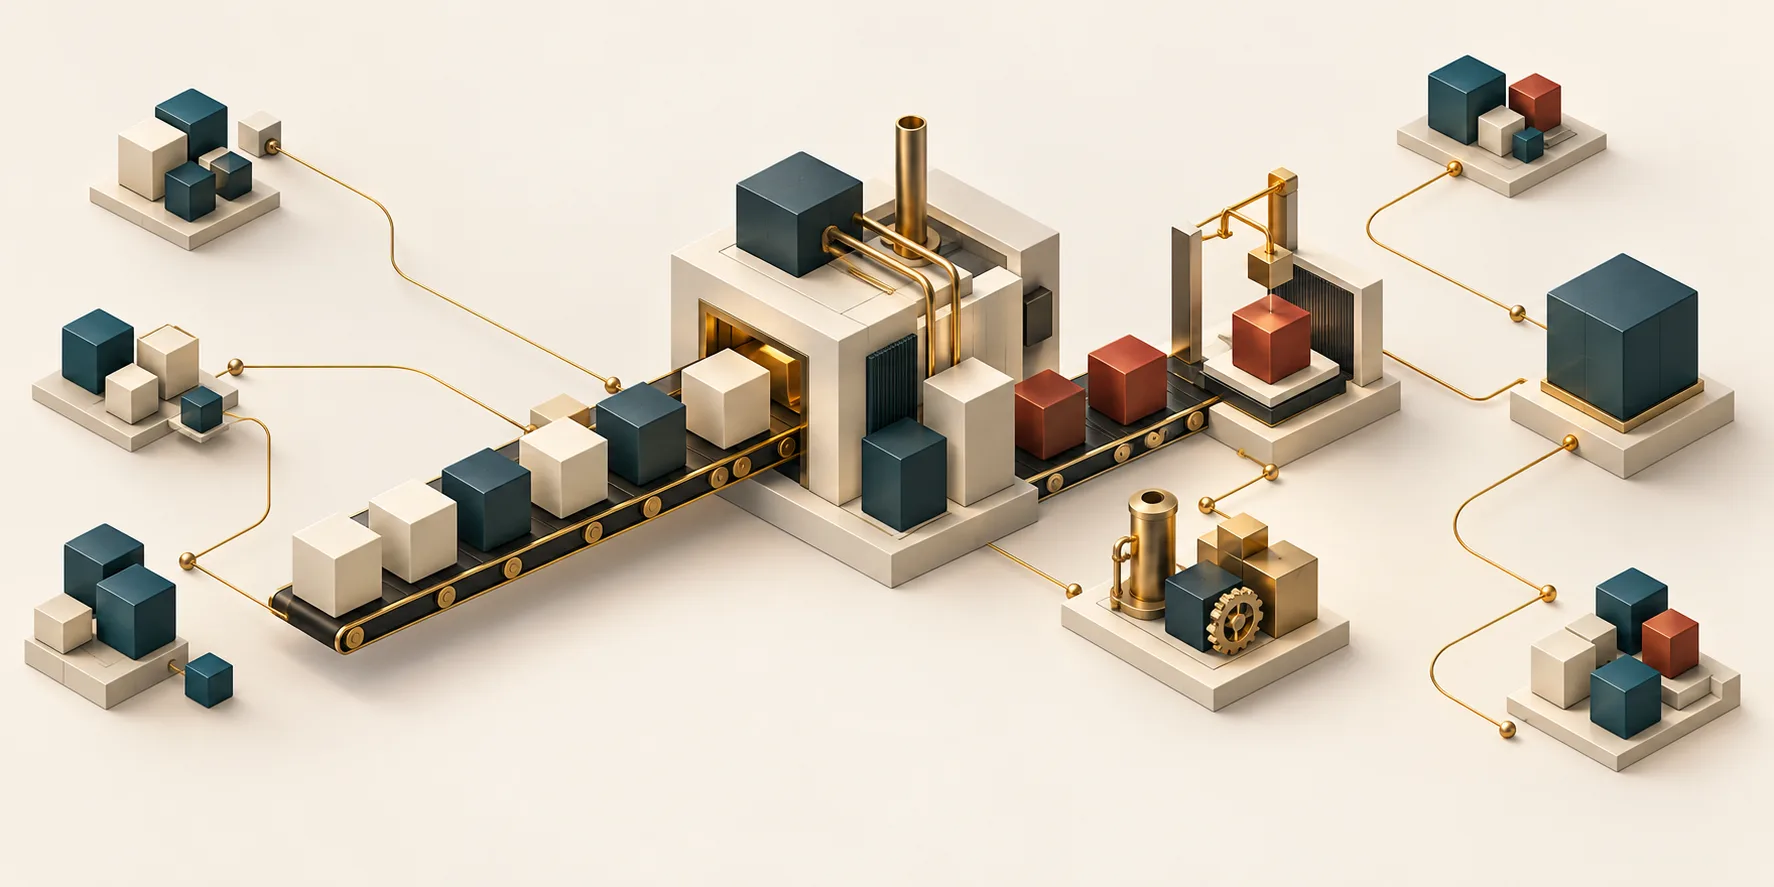
A manufacturer can have an ERP, machine data, and years of quality reports yet still struggle to answer a simple question: what happened to a particular production order? Before you buy an AI tool, follow a real order from customer request to shipment. The gaps you find will tell you which decisions software can support and which records people need to fix first.
Follow an order across the plant
Start with a recent production order that finished normally, then another that ran late or needed rework. Ask the planner to show the customer demand, promised date, bill of materials, routing, and released work order. Ask a supervisor what actually ran, on which line and shift, with which materials. Compare the planned start and finish with the events staff recorded on the floor.
Look for a shared identifier across the order, batch or serial number, operation, machine, and shipment. If a planner can connect them only by memory or a private spreadsheet, an AI system will inherit that guesswork. Check whether a material substitution, schedule change, or partial completion reaches the ERP promptly. A stock balance that reflects yesterday's shift can mislead a scheduling assistant today.
Write down each handoff and its owner. A small manufacturer may record a purchase order in the ERP, dispatch work from a board, and close production in a spreadsheet. You don't need to replace every tool to begin, but you do need to know which record has authority at each step and how late corrections reach other systems.
Join quality records to the work
Take the same orders into the quality process. Find the inspection plan and specification version that applied when the work ran. Then trace measurements, nonconformances, scrap, rework, concessions, and final release back to the batch or serial number. A pass/fail flag without the measured value, threshold, and time may hide an emerging problem. A report scanned weeks later may be sound evidence for an audit but too late for a live alert.
Ask who can correct a mistaken measurement and how the plant preserves the original entry. Check whether every failure has a disposition and whether the correction appears in the order's final yield. If you can't join a defect to its product, machine, process step, and material lot, an anomaly model won't tell the team what to inspect. NIST's industrial AI research treats equipment, execution, product quality, human feedback, and process data as different sources that manufacturers must evaluate together.
Read the maintenance history
Now take the machine that ran each order. Find its asset ID, downtime events, maintenance work orders, technician notes, replacement parts, and return-to-service approval. Check whether a fault code means the same thing across machines and whether operators record short stops at all. A note such as “fixed press” may help the next technician only if it says what failed, what they changed, and which asset they repaired.
Separate planned maintenance from breakdowns and production changeovers. These events interrupt work for different reasons. If a proposed predictive-maintenance system needs examples of failures, count how many verified events you have for the specific asset and failure mode. Months of sensor readings with no reliable failure labels won't prove that a model can warn you early. The first improvement may be a clearer work-order form and a common asset register.
Keep safety and control boundaries explicit. A maintenance assistant may retrieve approved procedures and similar work orders for a technician. It shouldn't tell a machine to restart or clear a lockout. The plant's authorized people must make those decisions under its established procedures.
Find the ERP boundary
The ERP often holds orders, inventory, purchasing, and cost. The shop floor may hold the current state of a job, while a quality system holds inspection evidence and a maintenance system holds asset history. For each field a proposed AI workflow needs, write down its source, owner, update delay, and permission rule. Don't treat a replicated dashboard as a live source if it refreshes only overnight.
Test five joins with actual records: customer order to production order; production order to material lot; production order to batch or serial number; batch to inspection result; and machine event to maintenance work order. Record the share of sampled cases that connect without manual interpretation. A missing common key, duplicate equipment ID, or mismatched unit of measure can break a workflow even when each application looks tidy on its own.
A NIST Manufacturing Extension Partnership case study describes a chemical manufacturer that linked controller output with its ERP and quality system to reduce manual entry and improve traceability. That case illustrates an integration path; it doesn't mean every plant needs the same software. NIST's manufacturing technology guidance describes system integration as a way to make data available to the people who need it.
Run a two-week readiness audit
Choose ten to twenty recent orders across product families, shifts, and outcomes. Include late orders, rework, and at least one equipment stoppage. The aim is to expose the ordinary exceptions that a polished demo leaves out. A planner, supervisor, quality lead, maintenance lead, and ERP owner can each show their part of the same cases. Avoid asking staff to create a fresh master spreadsheet before you have seen how they work today.
For every order, capture four results: whether the team can reconstruct its path, which joins require a person, how long the information takes to become current, and whether the record is trustworthy enough to guide an action. Log missing events and conflicting versions by source and owner. Sample size here is for discovery; it doesn't establish a plant-wide accuracy rate. If you need that rate for an investment decision, draw a larger representative sample.
End with a short map: authoritative systems and owners; broken identifiers or definitions; data access and safety boundaries; and a baseline for the chosen business outcome. Add the cost and time to repair the highest-value gaps. NIST's AI for Manufacturing programme focuses on fit-for-purpose methods, integration, traceability, and task-specific measures rather than a single model choice for every plant.
Choose a bounded first use case
Match the use case to the evidence you actually have. If order status is timely but machine failure labels are sparse, a read-only assistant that explains late orders from approved records is easier to test than a breakdown predictor. If inspection results link cleanly to batches, a quality team might test exception summaries that cite the underlying measurements. Keep a human responsible for release, rescheduling, and maintenance decisions.
Define success in plant terms before the pilot: fewer hours spent tracing a late order, faster identification of affected batches, less unplanned downtime, or fewer repeat defects. Compare the result with today's process, including staff review time and incorrect recommendations. A system that cannot identify the right order or show its source record should stay out of operational decisions until the data path is fixed.
For a regional manufacturer, readiness means you can explain where a record came from, how current it is, and who can act on it. That gives the business a sensible sequence: repair the joins that matter, test a narrow decision with real cases, and expand only when the outcome and safety checks hold on the plant floor.